very food processing plant manager knows what a stopped line sounds like. Whether it’s a guide rail wearing out, a roller cracking, a pad finally giving out or a mixing paddle breaking, downtime is measured in dollars per minute, not per hour. The usual solution of machining a replacement part or waiting for an OEM part that may no longer be available can take days or weeks. That’s usually not fast enough for a plant that runs 24/7.
That is where additive manufacturing, more commonly known as 3D printing, has become a practical tool in a food facility’s maintenance and engineering toolkit. It is not a replacement for injection molding, cast urethane production or machining, but a way to address urgent, low-volume problems that traditional methods were never designed to solve quickly. It’s also not just one technology anymore. Several types of 3D printing are now available for different kinds of jobs.
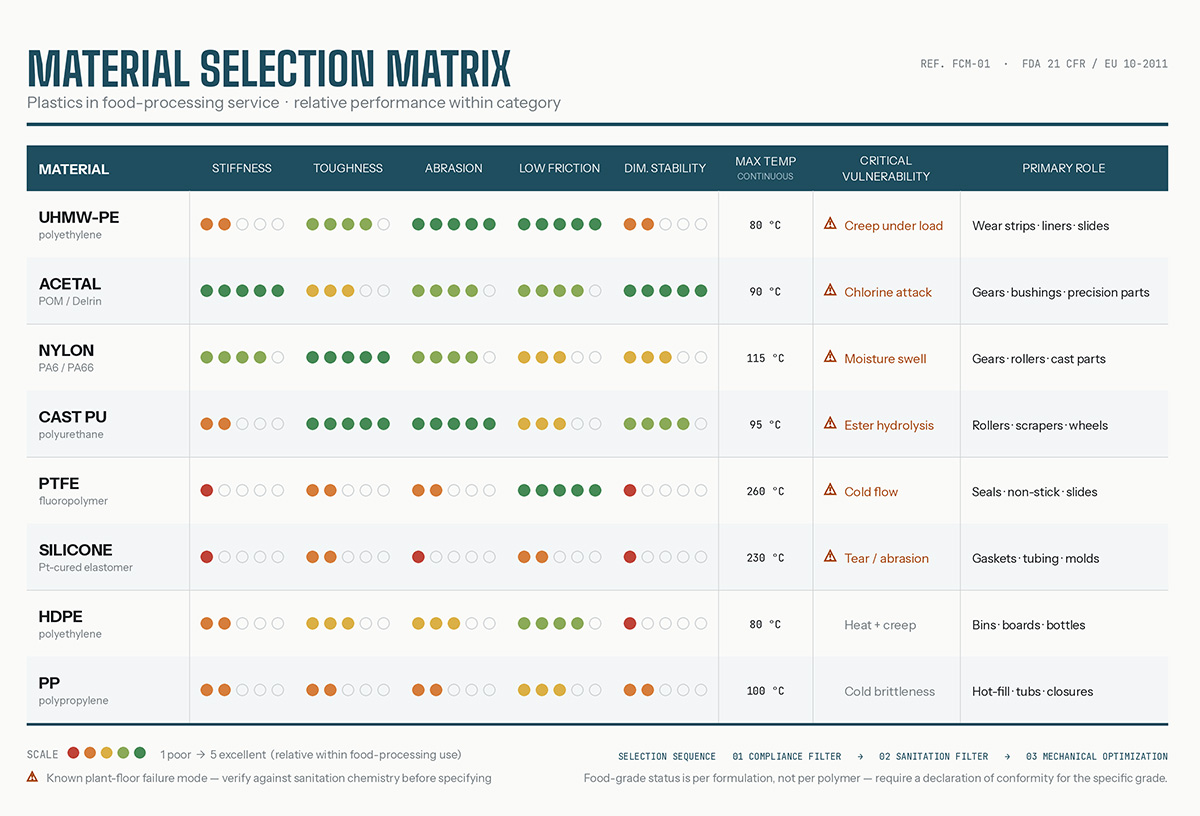
Stereolithography (SLA). This process uses UV light to cure liquid resin layer by layer to build parts. It produces components with fine detail, a clean surface and very tight tolerances, making it ideal for precision fixtures, guides and small mechanical parts where exact dimensions and a clean finish are important. There’s also a large selection of resins, from stiff and rigid materials to softer, rubber-like ones to heat-resistant grades, so one printer can cover parts with very different needs.
Fused deposition modeling (FDM) is the cheapest and most common type of 3D-printing. It builds parts by melting and depositing plastic filaments. It’s a good choice for low-stress jigs, fixtures and prototypes. Finish and accuracy aren’t quite as good as SLA, but materials like ABS, polycarbonate and nylon still perform reasonably well for parts not under heavy mechanical demand. It’s usually the least expensive way to print.
Selective laser sintering (SLS) and Multi Jet Fusion (MJF) use a bed of nylon powder that is fused together to create the part. No support structures are required during printing. These processes produce tougher, more durable parts that are closer to what you would expect from injection-molded nylon and are a good choice for functional parts like gears, brackets, housings and other components that need to survive real, ongoing use rather than just fit properly.
Each of these solutions comes with its own cost, turnaround time and durability, and choosing the right one is as much a matter of the part’s job as it is of price.
Instead, the broken gripper was reverse-engineered from directly from the physical part. Its shape was captured using measurement and scanning equipment, and from this data a CAD model was built that recreated the original design with some minor adjustments to improve durability and fit. Because this was a mechanical fixture and not a food-contact surface, the emphasis was on getting the proper dimensions and strength rather than food-safe resin chemistry.
For this part, SLA was chosen because of its tight tolerances and small features. It was made on a Form 4L using a standard engineering resin chosen for strength and dimensional stability. After printing, it then went through a simple finishing process of an isopropyl alcohol wash to remove uncured resin and a quick check to ensure everything fit before the part went back to the plant. A part with looser tolerances or one that needs to withstand greater impact might have been better suited for SLS or FDM. But that is really the point: It’s not about one printer or one material; it’s about selecting the right tool for the job.
From part breakage to a working replacement ready to fit, the whole process was completed in a fraction of the time that a traditional tooling and machining route would have taken. There was no tooling cost, no minimum order and no waiting in line at an outside machine shop. And because the part now exists as a CAD file, not just a worn-out sample, the next time it breaks, it can be swapped out even faster, no matter what printing process ends up being used.